


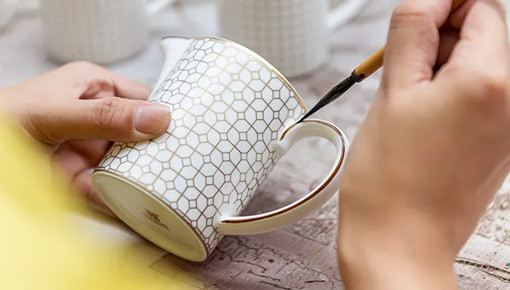

The Caliper Nobody Checks: Where the Numbers on Your Inspection Report Come From
A tolerance of two millimetres is not a property of a mug. It is a statement about two numbers, and each was produced by an instrument, in a room, held by a person with a reason to be quick. The tolerance is negotiated for a week. The instrument is assumed.
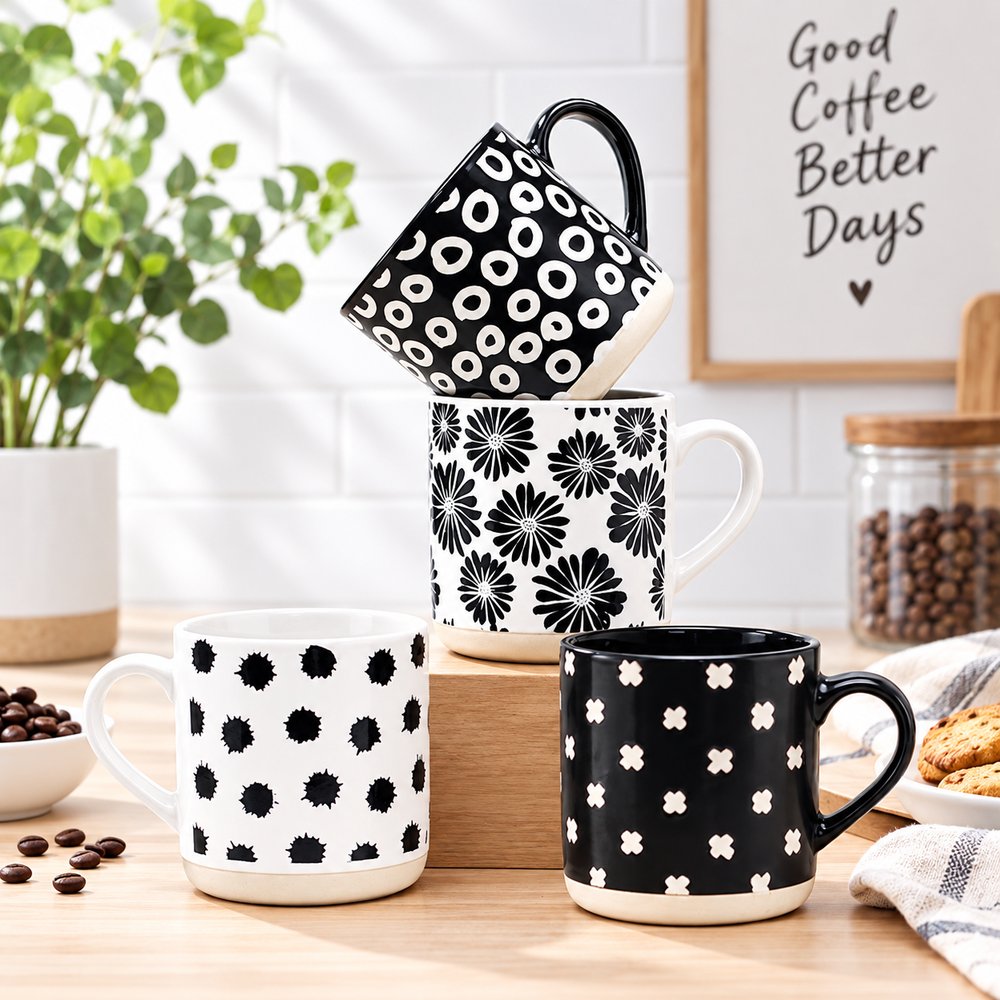
Products in this guide: Black and White Geometric Ceramic Mug · Ceramic Rice Bowl
Buyers audit the product, the process and the paperwork: a test report, an inspection standard, a sealed sample. The one link almost nobody examines is the tool that turned a mug into a figure: the caliper on the bench, the scale by the packing line, the cylinder used to check capacity, the template that decides whether a print has drifted. A factory can hold a valid certificate and still deliver a number that means very little, because a certificate answers a narrower question than most buyers think.
This is not an argument for distrusting measurements. It is an argument for knowing which ones you are relying on. Four instruments generate almost every figure in a ceramic order, each drifts in its own way, and each can be pinned down with a line of text. What follows is where those numbers come from, and what to write so that someone else can reproduce them.
Four instruments, and what each one decides
The caliper. Rim diameter, height, foot diameter, wall thickness at the rim. It is the instrument most often shared, most often dropped, and most often put away with its jaws closed on nothing. A caliper that has been dropped does not stop working. It starts lying by a small amount, always in the same direction.
The scale. Unit weight, and through it a proxy for wall thickness and for whether the body is the one you approved. It is the most reliable instrument in a ceramics plant, and the one most often standing on an unlevel bench, near a kiln door, or shared with the packing line.
The capacity measure. A graduated cylinder, or a weighed fill. Capacity is the specification that most often arrives out of tolerance, and the cause is usually not the mug but the method: where the water was stopped, at what temperature, and at which part of the meniscus it was read.
The go or no-go gauge. Rim profile, print-area boundary, decal position. Cheap to make, and the only one here that returns a decision instead of a number. A gauge turns a judgement into a pass or fail two people can agree on.
What a calibration record actually says
A calibration record states that an instrument was compared against a reference that can be traced to a national standard, on a given date, with a stated uncertainty. That is the whole of it.
It does not say the method was right. A correctly calibrated caliper used across the rim instead of across the diameter produces a wrong number with great confidence. It does not say the operator was trained, or that the reading was taken at the point the specification meant. Nor does it say the batch is good; it says one tool, on one day, sat close to a reference.
Which is why a certificate with no date, no uncertainty and no reference is a logo rather than evidence. Ask for both, and what the interval is based on. An instrument checked once a year is described at one moment, not on the other three hundred and sixty-four days.
Where a reading drifts
- Jaws worn or knocked, and a zero that was never reset before the session began.
- A scale on an unlevel bench, or one sharing a socket with a heat press.
- A cylinder read at the top of the meniscus instead of the bottom, by eye, at an angle.
- Water temperature, because the same volume does not read the same warm, and a rinse leaves the cylinder warm.
- A template washed, stacked or left in the sun until it no longer matches the print it was made for.
- A shared instrument with no record of who used it last, or on what.
None produces a large error. Each produces one about the size of the tolerance being argued about, which is why they end up in disputes and rarely in a root cause.
Capacity is the number that gets disputed
Two people measure the same mug and get 295 and 305 millilitres, and both are honest. One filled to the brim, the other to the fill line written in the specification. One read the meniscus at eye level, the other looked down into the cylinder.
This is why a capacity figure in an order needs three things beside the number: the fill level, the method and the instrument. Without them the figure is a claim that cannot be tested, and a rejection on capacity can always be answered with a piece that passes by another method.
When the tool and the batch disagree
If the factory reads 300 and your warehouse reads 290, the argument is not about the mug but about which measurement is the reference. Two instruments, a retained sample and a third reading settle it faster than correspondence.
This is where a physical reference earns its cost. A sealed sample with a recorded weight and capacity, held by both sides, turns an argument about method into a comparison against an object. The master sample guide explains how sealed references keep batches identical.
Four lines for the order
Written into the specification, measurement stops being a matter of habit. The spec freeze guide explains how artwork and packing files are locked between orders.
- The instrument and the method for each critical dimension, named rather than implied.
- The fill level, water temperature and reading convention for capacity.
- A calibration record for the instruments used on your order, with date and interval.
- The arbitration route when two measurements disagree, and who holds the reference sample.
One clause belongs in the signature block: who signs the release, and whether that person measured the ware. Where one person makes, measures and signs, the measurement carries an incentive. This needs no quality department, only that the signature means something.
The limit of this
A calibrated instrument does not make a good batch, and the paperwork described here will not catch a plant that measures carefully and fires badly. It closes a smaller gap: the one between a specification that assumes a number and a report that supplies one, with nothing checked in between.
When a figure is disputed and the product looks right, the instrument is worth a question. It is the cheapest part of the chain to check and the only part nobody has ever been asked about.
Related Products
Explore products featured in this guide:


Have questions? See our Sizes & Finishes FAQ and Ordering & Certifications FAQ.
Need a custom quote? Send an inquiry or browse our full product catalog.